THE PLANT
The operational plant dedicated to coating boasts a covered area of 12,000 sqm, optimized to manage complex workflows and high volumes, supported by 3,000 sqm of warehousing and 30,000 sqm of logistics areas.
COATABLE DIMENSIONS
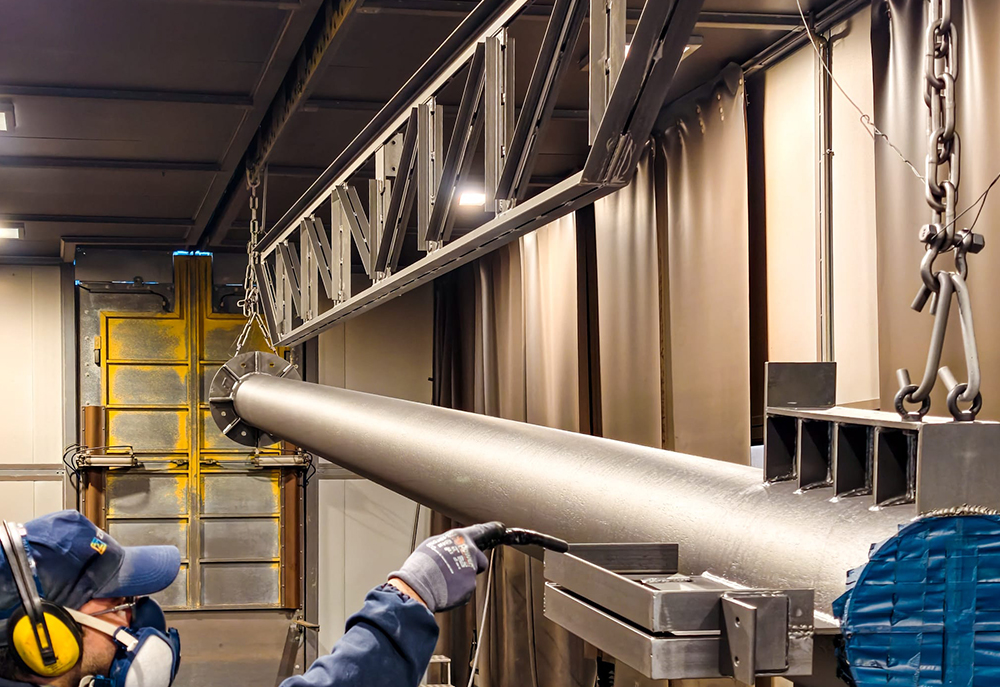
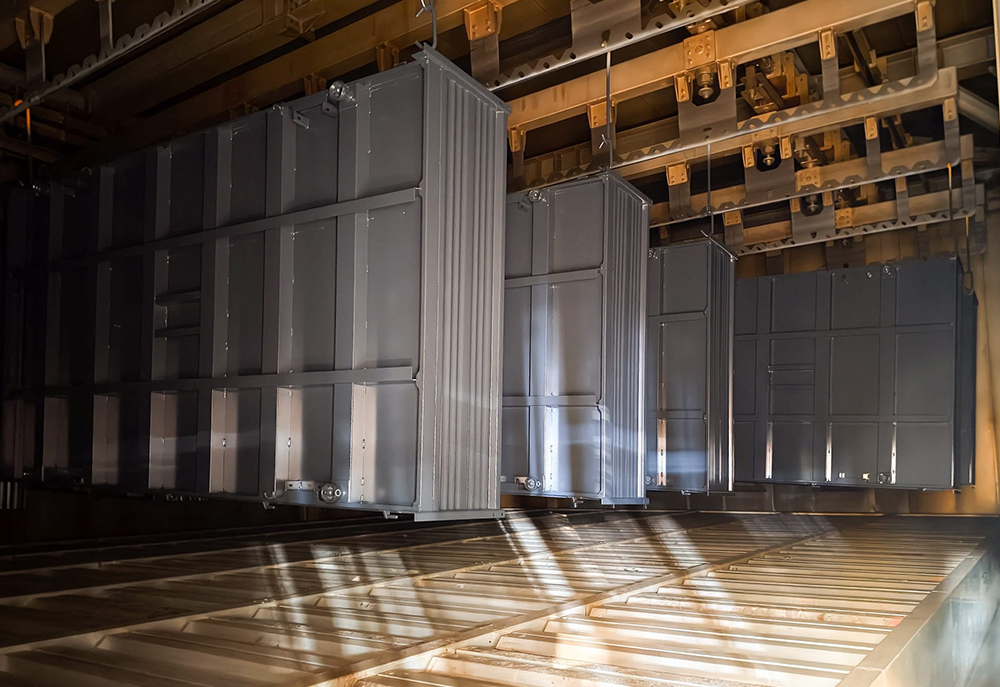
One of our competitive advantages is our ability to accommodate different product dimensions. The entire plant is designed around a versatile fixture, engineered to transport products through every stage of the production cycle — from pre-treatment to coating and post-process operations.
COATING MAXIMUM DIMENSIONS (AUTOMATED)
10.0 x 1.2 x 2.5 h m
SANDBLASTING MAXIMUM DIMENSIONS (AUTOMATED)
15.0 x 1.5 x 2.5 h m
FLIGHT BAR CAPACITY
3000 kg
TECHNOLOGY
Human skill, ingenuity, and experience are essential, but often they are not enough.
That is why we choose to invest in the finest tools capable of supporting our team of experts through every stage of the process. Innovation and functionality, paired with a strong focus on sustainability and waste reduction, are the driving principles behind the design of our technological cycle, positioning us as an industry benchmark.
Commitment to Sustainability: An Efficient Model
Vernix’s technological innovation is inextricably linked to environmental responsibility, through targeted solutions designed for energy efficiency and drastic waste reduction.
Clean Energy
The integration of an advanced photovoltaic system guarantees constant coverage of part of the company’s energy needs. This investment in renewable sources powers the production processes while significantly reducing the carbon footprint and overall environmental impact of the entire facility.
Water and Chemical Management
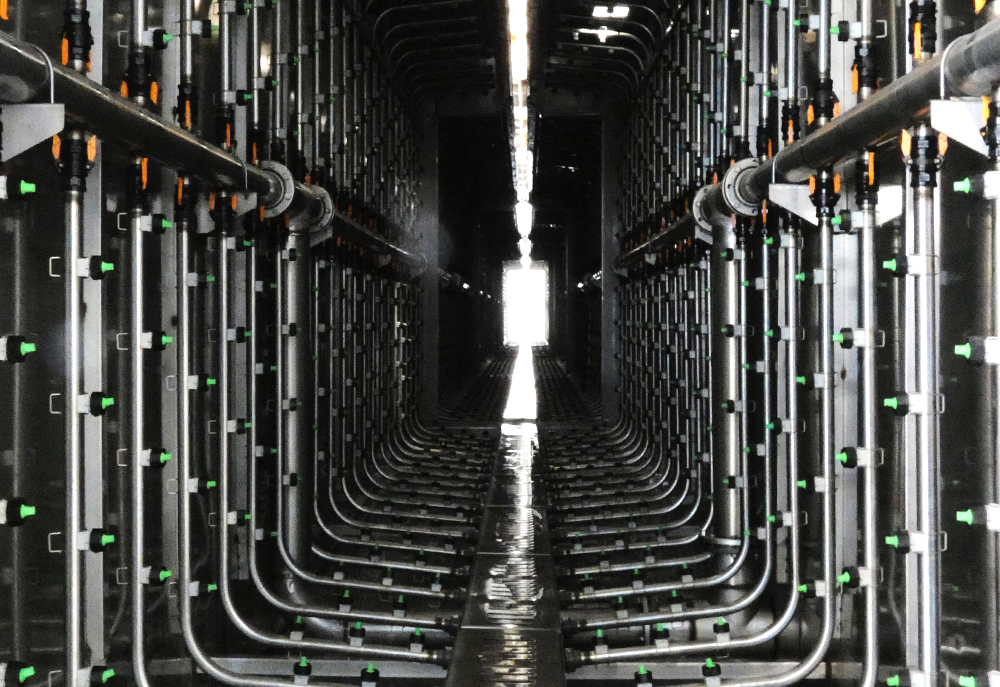
The chemical washing tunnel operates as a completely closed-loop system, using exclusively water treated by an internal purification plant for wastewater recovery. This system eliminates constant water extraction from the public network, ensuring a fully eco-sustainable metal pre-treatment cycle.
Zero Waste and Thermal Savings
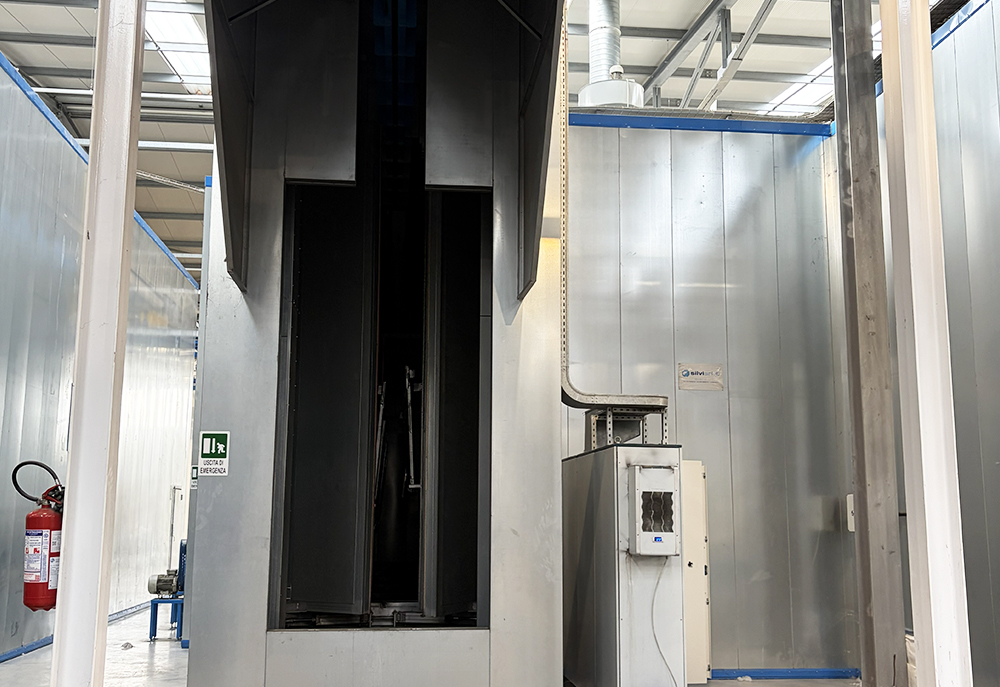
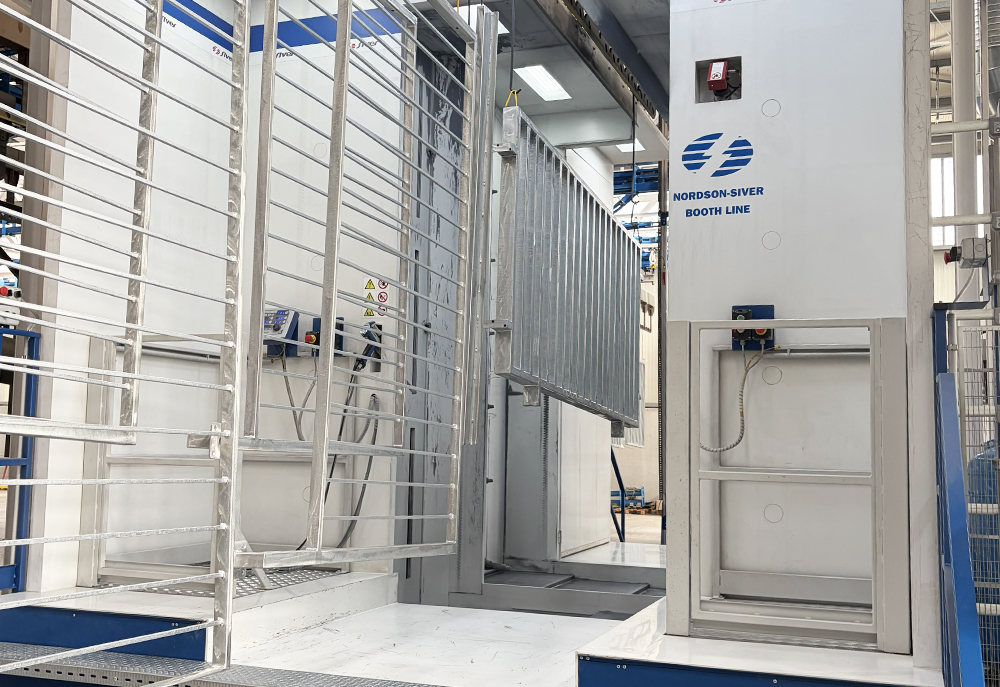
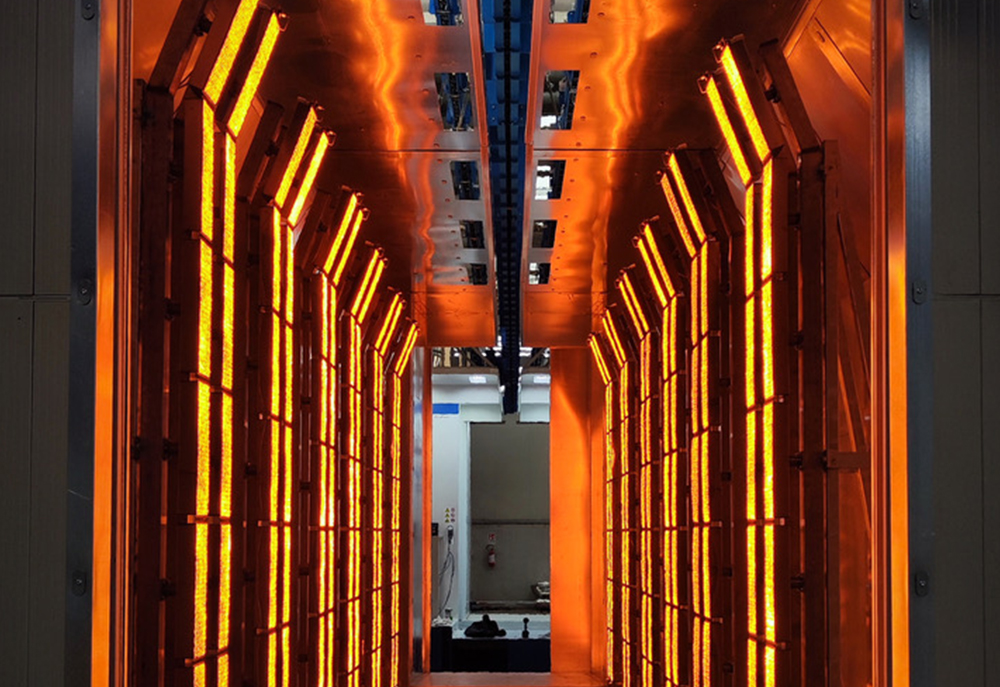
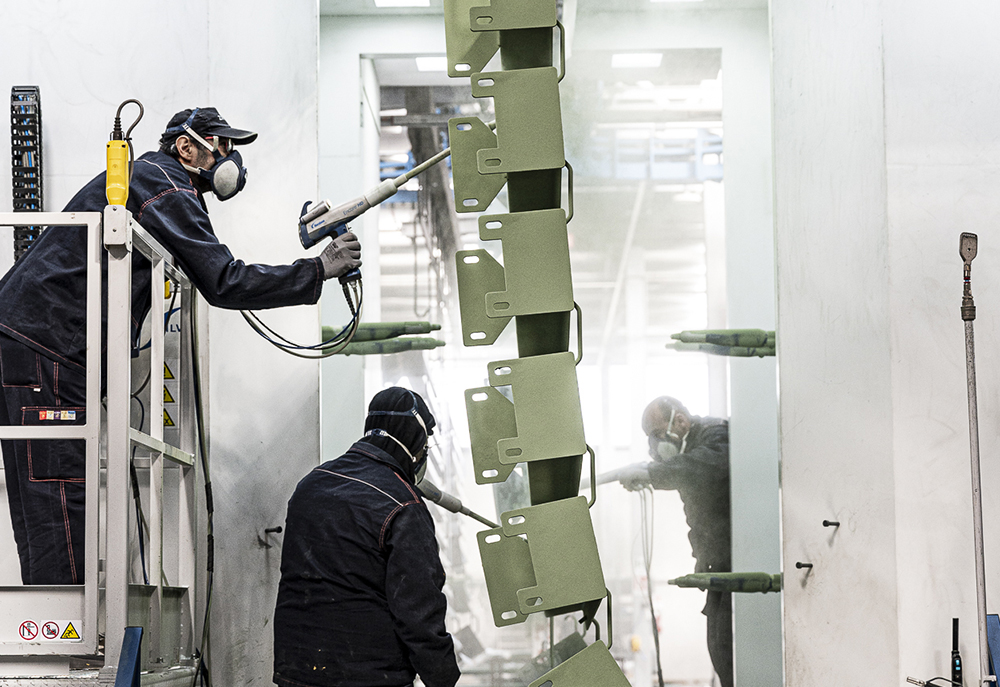
The primer booth fully recycles powders to eliminate waste, while the dedicated oven utilizes intelligent panels that activate only when the product passes through. This technology ensures absolute precision, delivering both energy savings and a reduction in industrial waste compared to traditional systems.